

도난 방지 나사는 누군가가 그것을 꺼내려고 하는 순간까지 일반 고정 장치처럼 보입니다. 차이점은 드라이브 홈에 있습니다. 필립스 십자 또는 일반 육각 소켓 대신 헤드가 일상적인 도구에 맞지 않는 모양을 갖습니다. 이러한 단일 설계 결정으로 저렴한 나사가 작지만 효과적인 억제 수단으로 바뀌었습니다. 이것이 바로 변조 방지 패스너가 번호판, 자동 판매기, 리프트 패널, 거리 조명 및 ......
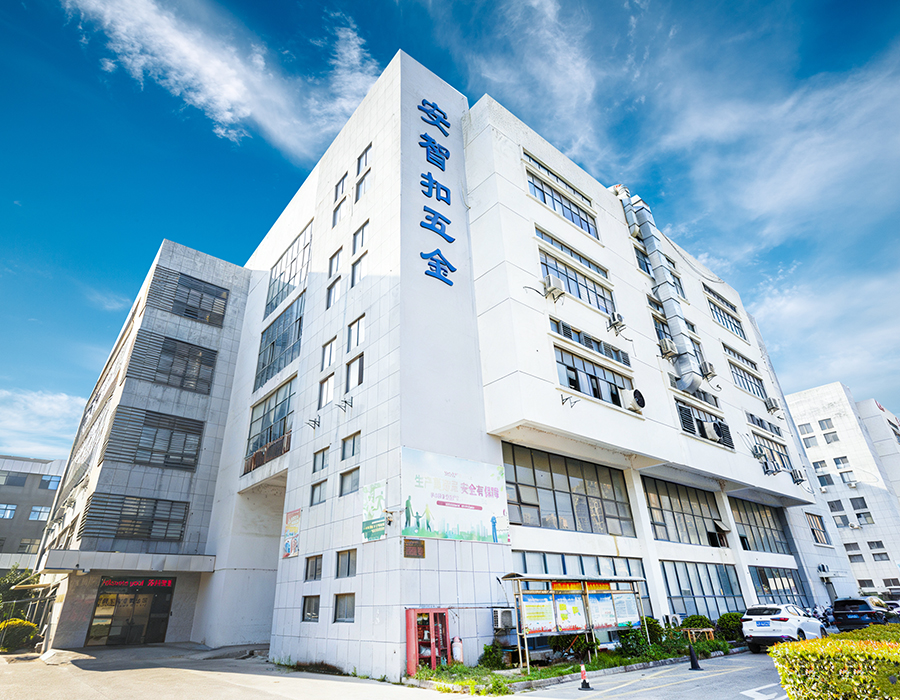
더 읽기Suzhou Anzhikou Hardware Technology Co., Ltd. 는 정밀 나사의 개발, 생산 및 판매를 통합한 제조업체입니다. 와셔 제조업체 및 와셔 공장 중국에 위치회사의 기존 공장은 2,000제곱미터 면적을 차지하며, 냉간 압조, 나사산 롤링 와이어, CNC 및 풀림 방지 등 체결구 생산 장비를 포함하여 대만과 일본에서 200세트 이상의 정밀 장비를 도입했습니다. 외경 0.6mm/길이 0.6mm의 초소형 나사를 생산할 수 있으며, 표준 부품 및 비표준 나사의 연간 생산 능력은 최대 2,000제곱미터입니다.
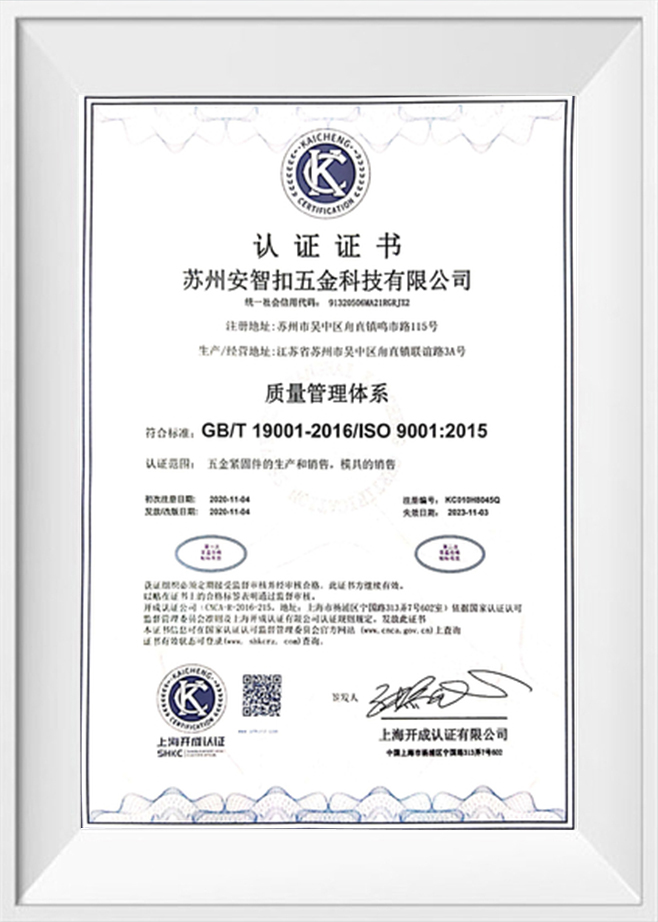
안즈커우 하드웨어는 완벽한 테스트 장비를 갖추고 ISO9001:2015 품질 시스템 인증을 통과했으며, 20년의 산업 생산 및 개발 경험, 20년의 업계 경험을 가진 엔지니어링 및 기술 직원 10명이 고객 요구에 따라 다양한 비표준 나사를 맞춤 제작합니다. 도매 와셔고객의 다양한 품질 및 수량 요구를 충족시킵니다. 쑤저우 안즈커우 정밀 나사는 우수한 제품 품질로 전 세계 40개국 및 지역에 수출되고 있습니다.
도난 방지 나사는 누군가가 그것을 꺼내려고 하는 순간까지 일반 고정 장치처럼 보입니다. 차이점은 드라이브 홈에 있습니다. 필립스 십자 또는 일반 육각 소켓 대신 헤드가 일상적인 도구에 맞지 않는 모양을 갖습니다. 이러한 단일 설계 결정으로 저렴한 나사가 작지만 효과적인 억제 수단으로 바뀌었습니다. 이것이 바로 변조 방지 패스너가 번호판, 자동 판매기, 리프트 패널, 거리 조명 및 ......
더 읽기서스펜션 컨트롤 암을 변경하거나, 트레일러 프레임을 제작하거나, 공정 라인에서 플랜지를 조이는 중이고 3/4-10 볼트가 토크 사양을 기다리고 있습니다. 가장 직접적인 대답은 3/4-10 볼트는 등급과 상태에 따라 약 150~400lb-ft의 토크를 가할 수 있다는 것입니다. 볼트가 2등급인 경우 건조 상태에서 약 150lb-ft를 사용합니다. 8등급인 경우 약 400lb-ft 건......
더 읽기분주한 기계 공장에서 최종 조립 과정에서 마지막으로 발견하고 싶은 것은 소켓 헤드 캡 나사 카운터보어를 자랑스럽게 생각하는 0.010인치 위치입니다. 한 유지보수 엔지니어가 표준 카탈로그에서 주문한 1/4-20 SHCS에 관해 우리에게 연락한 적이 있습니다. 나사산 피치는 맞았으나 헤드 높이가 접근 가능한 공간을 초과했고 육각 키가 소켓에서 헐거워진 느낌이 들었......
더 읽기배달 밴에서 번호판이 밤새 사라졌습니다. 누군가가 동전으로 모든 고정 장치를 빼냈기 때문에 화장실 칸막이가 헐거워졌습니다. 대중교통 대피소는 이번 분기에 세 번째로 접근 패널을 잃었습니다. 세 가지 경우 모두 나사의 강도가 문제가 아니라 표준 일자형 드라이버나 Phillips 드라이버가 머리에 맞는 문제입니다. 그렇다면 최고의 보안 나사는 하나의 보편적인 부품이 아닙니다. 이는 변......
더 읽기A fender conical washer functions as a disc spring whose load-deflection curve is governed by the cone angle, material thickness, and the ratio of outer to inner diameter. Suzhou Anzhikou Hardware Technology Co., Ltd. manufactures fender conical washers with cone angles ranging from 4 to 8 degrees, where the lower angles produce flatter spring rates suitable for thermal expansion compensation, and steeper angles generate higher spring constants for vibration isolation. The spring rate k of a conical washer follows the relationship k ∝ t³/(Dₒ - Dᵢ), meaning that a 20% increase in material thickness increases stiffness by 73%. This cubic sensitivity makes thickness control the dominant quality parameter in washer production.
Anzhikou Hardware's Taiwan-imported stamping and forming equipment maintains material thickness variation within ±0.02mm on washers from 0.3mm to 3.0mm thickness. For a typical M8 fender conical washer with 24mm outer diameter, 8.4mm inner diameter, and 1.5mm thickness in 65Mn spring steel, this thickness control translates to a spring rate tolerance of ±8%. The company's 200-plus precision machines include automated thickness gauging stations that reject washers where thickness deviation exceeds ±0.015mm, preventing the stack-up of out-of-tolerance parts that would cause uneven load distribution in multi-washer assemblies. The 2000-square-meter facility houses these production lines alongside the cold heading and thread rolling equipment, enabling integrated supply of washers with mating screws and nuts.
| Washer Specification | Cone Angle (°) | Thickness (mm) | Solid Height Load (N) | Recommended Deflection Range (mm) |
| M6×18 OD | 4 | 0.8 | 1,850 | 0.15 - 0.35 |
| M8×24 OD | 6 | 1.2 | 4,200 | 0.25 - 0.55 |
| M10×30 OD | 8 | 1.8 | 8,600 | 0.40 - 0.80 |
| M12×37 OD | 6 | 2.5 | 15,400 | 0.50 - 1.00 |
Operating a fender conical washer beyond its solid height load causes plastic deformation known as "setting," permanently flattening the cone and eliminating spring action. Anzhikou Hardware's engineering team of 10 technicians with 20 years of industry experience recommends specifying washers with a solid height load at least 1.5 times the maximum expected working load, providing a safety margin against over-torquing during assembly. For applications where torque-controlled tools are unavailable, the company supplies washers with color-coded thickness bands that allow visual verification of correct specification before installation.
The material of a fender conical washer determines not only its spring rate but also its fatigue life, corrosion resistance, and maximum operating temperature. Suzhou Anzhikou Hardware Technology Co., Ltd. produces these washers in 65Mn spring steel, 304 stainless steel, and phosphor bronze (CuSn6), with each material demanding distinct forming and heat treatment parameters. 65Mn, containing 0.65% carbon and 1.0% manganese, achieves the highest spring rates and fatigue limits after quenching and tempering to 42-48 HRC. However, this hardness makes the material susceptible to hydrogen embrittlement if electroplated without proper baking.
The company's 2000-square-meter facility includes continuous belt furnaces for austenitizing 65Mn washers at 830°C followed by oil quenching and tempering at 400°C. This heat treatment cycle produces a tempered martensite microstructure with tensile strength of 1,600 MPa and yield strength of 1,400 MPa. For export orders to European automotive manufacturers—among the 40 countries and areas served—Anzhikou Hardware performs de-embrittlement baking at 200°C for 4 hours within 1 hour of zinc plating, conforming to VW 60250 and PSA B15 5202 standards.
Multiple fender conical washers can be assembled in stacked configurations to achieve load-deflection characteristics unavailable from single washers. Suzhou Anzhikou Hardware Technology Co., Ltd. provides stacking guidance based on the company's 20 years of experience in non-standard screw customization, recognizing that improper stacking negates the washer's spring function and can induce bolt bending moments. The two fundamental arrangements—parallel stacking (nested cones facing the same direction) and series stacking (alternating cone orientation)—produce dramatically different system behaviors.
In parallel stacking, n washers nested together increase the effective thickness by factor n while maintaining the same cone angle. The combined spring rate becomes n times the single washer rate, and the total deflection capacity remains equal to a single washer. This arrangement suits applications requiring high load capacity with limited axial space, such as preloading bearings in precision spindles. Anzhikou Hardware recommends limiting parallel stacks to three washers because nesting beyond this number causes the innermost washer to bear disproportionate load due to friction between adjacent cones, creating load distribution unevenness of 15% or more.
| Stack Configuration | Number of Washers | Combined Spring Rate | Total Deflection Capacity | Typical Application |
| Single | 1 | k | δ | General clamping |
| Parallel | 2 | 2k | δ | Bearing preload |
| Series | 2 | k/2 | 2δ | Thermal expansion compensation |
| Series-Parallel | 4 (2 pairs series, then parallel) | k | 2δ | Valve spring retainer |
Series stacking, with washers oriented alternately, increases deflection capacity by factor n while reducing the combined spring rate to k/n. This configuration is essential for thermal expansion joints where the bolted connection must accommodate large axial displacements without load variation. Anzhikou Hardware's engineering team calculates the required washer stack based on the thermal expansion differential between bolt and flange materials, the operating temperature range, and the permissible clamping load variation. For a steel bolt securing an aluminum flange across a 100°C temperature swing, a series stack of three M10 fender conical washers maintains clamping force within ±10% of the initial value, compared to ±35% variation with a rigid joint.
The coefficient of friction between a fender conical washer and the mating surfaces directly affects the torque-tension relationship of the bolted joint. A high friction coefficient requires greater torque to achieve target clamping load, increasing torsional stress in the bolt and the risk of thread galling. Suzhou Anzhikou Hardware Technology Co., Ltd. controls surface finish on its washers to manage this friction, with roughness values and coatings selected based on the specific assembly requirements rather than applying universal finishes.
Bare 65Mn steel washers with a mill scale surface exhibit friction coefficients of 0.18 to 0.22 against steel flanges. After shot peening to Ra 3.2μm, this increases to 0.25 to 0.30 due to mechanical interlocking of surface asperities. For applications requiring predictable torque-tension relationships, Anzhikou Hardware applies manganese phosphate coatings that reduce the friction coefficient to 0.12 to 0.15 while providing 48-hour salt spray protection. The phosphate layer's microcrystalline structure acts as a lubricant reservoir, retaining assembly grease that would otherwise be squeezed from the interface during tightening.
The company's ISO9001:2015 quality system verifies friction consistency through torque-tension testing on representative washer samples. Each production lot is tested with a calibrated bolt tightened to 75% of proof load, measuring the resulting clamping force. Variation exceeding ±10% from the nominal torque-tension curve triggers process investigation into surface finish, coating thickness, or material hardness deviations.
Fender conical washers with outer diameters below 6mm—typically mating with M2 or smaller screws—present manufacturing challenges that scale non-linearly with size reduction. The cone forming operation requires die clearances of 0.01 to 0.02mm, and material thickness variations that would be negligible on M10 washers become proportionally significant. Suzhou Anzhikou Hardware Technology Co., Ltd. produces miniature fender conical washers down to 3mm outer diameter for electronics and medical device applications, leveraging the same precision capabilities that enable miniature screw production down to 0.6mm diameter.
The blanking operation for miniature washers employs compound dies that pierce the center hole and blank the outer profile in a single stroke, maintaining concentricity within 0.03mm. Anzhikou Hardware's Japan-imported stamping equipment achieves this through guided pillar die sets with preloaded ball bearings that eliminate lateral play. The cone forming stage uses polyurethane pressure pads rather than steel strippers to avoid marring the delicate washer surfaces; the elastic pad applies uniform pressure during forming and retracts without scratching during part ejection.
For 65Mn miniature washers requiring heat treatment, the company employs vacuum furnaces rather than atmosphere furnaces to prevent oxidation scaling that would alter the surface finish and friction coefficient. The vacuum level is maintained below 10⁻³ mbar during austenitizing, with nitrogen backfilling during cooling to achieve a bright surface. This process, developed through 20 years of industrial production experience, eliminates the acid pickling that would otherwise be required for atmosphere-processed parts—a critical consideration for medical device washers where residual acid ions could compromise biocompatibility.
Quality inspection of miniature fender conical washers employs optical comparators with 50× magnification and rotary staging that measures cone angle at 12 positions around the circumference. The complete range of testing equipment at Anzhikou Hardware's facility includes laser micrometers that scan washer profiles at 0.1-degree angular resolution, detecting cone angle variations as small as 0.2 degrees that would cause uneven seating. This inspection capability supports the company's annual production capacity of 2,000 square meters by preventing defective parts from entering assembly operations where they would be difficult to detect and expensive to remove.
When a fender conical washer is used under the head of a screw securing thin sheet metal, the conical bearing surface distributes load radially outward rather than concentrating it at the hole edge. However, if the washer outer diameter is too small relative to sheet thickness, the sheet material yields beneath the cone and creates a permanent dimple that reduces clamping effectiveness. Suzhou Anzhikou Hardware Technology Co., Ltd. provides sizing guidelines based on elastic foundation theory, where the washer outer diameter should exceed 4 times the sheet thickness for steel sheets and 5 times for aluminum sheets to maintain elastic contact.
| Sheet Material | Thickness (mm) | Minimum Washer OD (mm) | Recommended Screw Size | Max Clamping Load Before Dimpling (N) |
| Steel (DC04) | 0.8 | 12 | M4 | 2,400 |
| Steel (DC04) | 1.2 | 16 | M5 | 3,800 |
| Aluminum (5754) | 1.5 | 20 | M6 | 2,200 |
| Aluminum (5754) | 2.0 | 24 | M8 | 3,600 |
Edge lift occurs when a washer is positioned too close to the sheet edge—typically within 1.5 times the washer outer diameter—causing the sheet to bend upward rather than compress uniformly. Anzhikou Hardware's engineering team reviews customer assembly drawings during the non-standard screw customization process to identify edge proximity risks and recommend washer sizes or flange reinforcements. For automotive body panel applications where edge distances are constrained by styling requirements, the company produces fender conical washers with extended outer diameters and reduced thicknesses that increase the bearing area without increasing spring rate beyond the bolt's capacity.
The company's business philosophy of "quality first, continuous innovation, optimize costs, improve speed" manifests in washer production through continuous die improvement programs. Recent innovations include the adoption of finite element simulation for cone forming die design, reducing trial-and-error die development time from 3 weeks to 5 days. This capability enables rapid response to custom washer inquiries from the 40 countries and areas in Anzhikou Hardware's export portfolio, supporting the company's commitment to provide high quality, high precision fasteners products with professional service and on-time delivery.
연락처 정보

주소:아니요. 중국 장쑤성 쑤저우시 우중구 루즈진 창홍베이 도로 248-2호.
전화:+86-13913588597
제품
모바일 터미널


